System reference
Gripper for cast parts
System solutions | Mechanical and plant engineering | Metal | Foundry

Challenge
A large machining center of a robot manufacturer needed to be able to be operated without staff over two shifts. The long processing time of up to 45 minutes for a component needed to be used to deburr the components during the non-productive time.
Solution
Eight parts each are provided on a parts buffer. A tool changer can change to either the gripper for part 1 (rocker) or gripper 2 (carousel). During the non-productive time, the tool changer brings in a deburring spindle. The clamping time was reduced from 40 min. (for manual clamping) to 2 min. (automatic clamping). The part yield was increased many times over and the parts leave the system deburred.
Highlights and technical data
 IP40
 Pneumatic
 External gripping
 Internal gripping
 Gripping force safety device for spring
Technical Data
| Drive type | PNEU |
| Max. gripping force | 34000 [N] |
| Gripping concept | FORM |
| Gripping safety device | FED |
| Max. stroke | 30 [mm] |
| IP class | IP40 |
| System weight | 131 [kg] |
| Max. workpiece weight | 160 [kg] |
| Max. workpiece temperature | 80 [°C] |
Built-in standard components
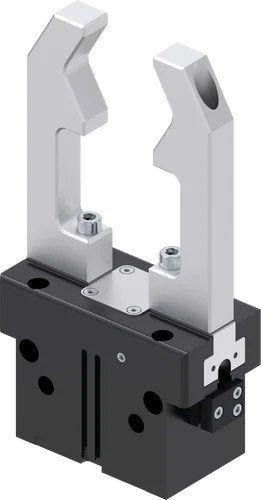
2-Jaw Parallel Grippers
Series GP400
pneumatic
Stroke per jaw
2 mm - 30 mm
Gripping force
85 N - 19275 N
Gripper finger length
50 mm - 300 mm
Maintenance-free cycles max.
10 million
IP class
IP40
Weight
0.076 kg - 17 kg
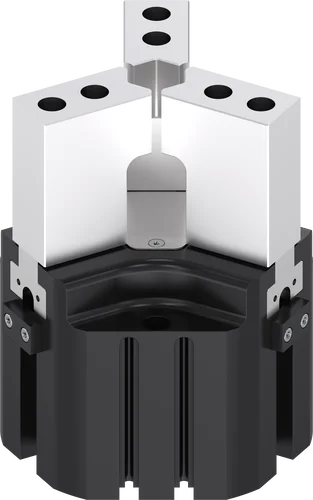
3-Jaw Concentric Grippers
Series GD300
pneumatic
Stroke per jaw
2 mm - 30 mm
Gripping force
200 N - 34150 N
Gripper finger length
50 mm - 250 mm
Maintenance-free cycles max.
10 million
IP class
IP40
Weight
0.14 kg - 26 kg
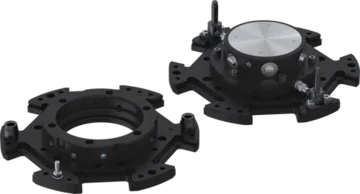
Tool Changers
Series WWR1000
pneumatic
Connecting flange according EN ISO 9409-1
160 / 200
Electrical energy transfer
optional
Locking stroke
1 mm
Weight
5.3 kg - 15 kg
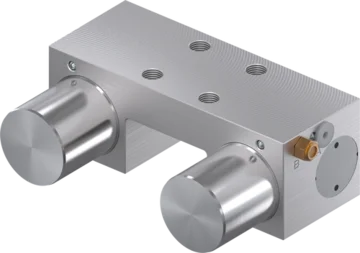
Clamping element
Series MKS
Profile rail guide
Holding force
145 N - 1450 N
Theoretical holding force (µ=0,1)
313 N - 1813 N
Operating pressure
4 bar - 6.5 bar
Weight
0.21 kg - 3.2 kg
Clean room class
6